
Whilst working asPrototype modelsIn this industry, the choice of manufacturing process plays a decisive role in the accuracy, cost, lead time and performance of prototypes; it is, in fact, a crucial factor in a company’s R&D decision-making. Following decades of development, prototype manufacturing has evolved into a process centred on CNC precision machining,3D printingRapid prototyping,Vacuum CastingThese are the three main manufacturing processes. Each of these processes has its own advantages and disadvantages, and each fulfils a different role in adapting to prototype production under different scenarios and requirements. For businesses, only by accurately understanding the characteristics, differences and limitations of these three processes can they select the optimal solution, thereby enabling prototype models to deliver their maximum value. This article will provide an in-depth analysis of the three core prototyping processes from four key perspectives—process principles, strengths and weaknesses, material suitability, and application scenarios—to offer industry professionals a comprehensive reference.
I. CNC Precision Machining: The “Gold Standard” for High-Precision Prototypes”
CNC machining is the most widely used and mature process in the prototype modelling industry; it is hailed as the “gold standard for high-precision prototypes”. Its core principle lies in the use of computer programming to generate G-code, which is then used to control three-axis, four-axis and five-axis CNC machining centres to perform precise cutting on block-shaped blanks made of plastics, metals and other materials, gradually removing excess material to ultimately produce a prototype that meets the design specifications.
Key strengths:
Extremely high accuracy, CNC machiningAccuracy can range from ±0.02 to 0.05 millimetres; some five-axis machines can even achieve an accuracy of ±0.01 millimetres. It is the most precise option among all prototype manufacturing processes and is perfectly suited to meeting the ultra-high precision requirements of sectors such as aerospace, automotive and medical devices.
It is compatible with an extremely wide range of prototype materials, covering virtually all commonly used prototype materials, including plastics such as ABS, as well as PC, POM and acrylic, It also supports metal materials such as aluminium alloy, stainless steel, copper and titanium alloy. It performs particularly well when machining high-strength, high-hardness metals—something 3D printing simply cannot match.
Offering outstanding performance, CNC prototypes are machined from solid material, meaning their structural strength is identical to that of mass-produced products, and their mechanical properties are exactly the same as those of mass-produced products. their heat resistance is entirely consistent with that of mass-produced products, and their corrosion resistance is exactly the same as that of mass-produced products. They can therefore be subjected directly to rigorous functional validation tests, including assembly testing, strength testing and environmental testing.
Post-processing is straightforward; the surface achieves a high degree of smoothness after processing and has an excellent texture. A variety of finishes—including high-gloss, matt, sandblasted and electroplated—can be easily achieved, and there is no difference in appearance or texture compared to mass-produced items.
Weaknesses and shortcomings:
The costs are relatively high; the investment in equipment is substantial, the time required for programming is considerable, and material utilisation is relatively low. Consequently, the cost per unit for small-batch prototypes is numerically higher than that of processes such as 3D printing.
It features internal hollow sections, complex curved surfaces and irregularly shaped cavities, as well as some small, deep holes. Given these structural characteristics, CNC machining presents extreme difficulties and may even be impossible.
The production cycle is rather lengthy; the processes involved—including programming, fixturing, rough machining and finish machining—are extremely intricate. Typically, the production cycle for a complex prototype takes between two and five days.
Use cases:
CNC machining is the preferred method for producing metal prototypes that are large in size, high in strength and high in precision. It is primarily used in the following areas: structural components for new energy vehicles, engine parts and gearbox housings; precision components for medical devices and surgical instruments; components for aerospace vehicles and structural parts for satellites; housings for industrial equipment and joints for robotic arms; as well as mid-frames and casings for consumer electronics – all of which place extremely high demands on precision, strength and surface finish.

II. 3D Printing Rapid Prototyping: The “King of Efficiency” for Complex Structural Prototypes”
Additive manufacturing, also known as 3D printing, is a revolutionary prototyping technique that has emerged over the past decade. Its core principle is based on the concept of “layered build-up”, whereby a 3D model is sliced, and then using methods such as laser, hot-melt or photopolymerisation to build up the material layer by layer to form the final shape. The mainstream 3D printing technologies currently used in the prototyping industry include SLA (stereolithography), SLS (selective laser sintering), FDM (fused deposition modelling) and MJF (multi-jet fusion).
Key strengths:
Unlimited design possibilities: It places no constraints on machining techniques and can easily produce complex configurations that cannot be achieved through CNC machining—such as those featuring cavities, thin walls, irregularly shaped surfaces, internal interconnected passages, structures with numerous holes, and monolithic assembled components—making it ideally suited to the requirements of innovative designs and complex products.
It is extremely fast; no programming, clamping or tool changes are required. Once a 3D model has been imported, it can be printed automatically. Simple prototypes can be produced within a few hours, whilst complex prototypes can be delivered within one to two days. Its efficiency far exceeds that of CNC machining, making it the ideal choice for rapid prototyping and urgent requirements.
With high material utilisation, low unit costs for small batches, no need for tooling, and costs kept under control, this approach is particularly well-suited to small-batch prototypes of 1–10 pieces, enabling companies to significantly reduce their R&D costs.
Offering a high degree of design flexibility, it supports customisation and allows for the simultaneous development of multiple versions; designers are free to give full rein to their creativity without having to worry about manufacturing constraints.
Weaknesses and shortcomings:
The typical accuracy of 3D printing is generally around plus or minus 0.1 to 0.2 millimetres, which is on the low side; it is lower than that of CNC machining. Layer lines are clearly visible, and the surface requires careful sanding as part of the post-processing.
There are differences in performance; 3D-printed parts have a layer-by-layer structure, and their mechanical properties, heat resistance and strength are slightly lower than those of solid machined parts. Furthermore, some high-performance materials are not suitable for this process.
There are specific dimensional constraints; as these are dictated by the moulding capacity of the equipment, large-scale prototypes need to be split into sections and reassembled, which affects both the overall accuracy and strength.
Use cases:
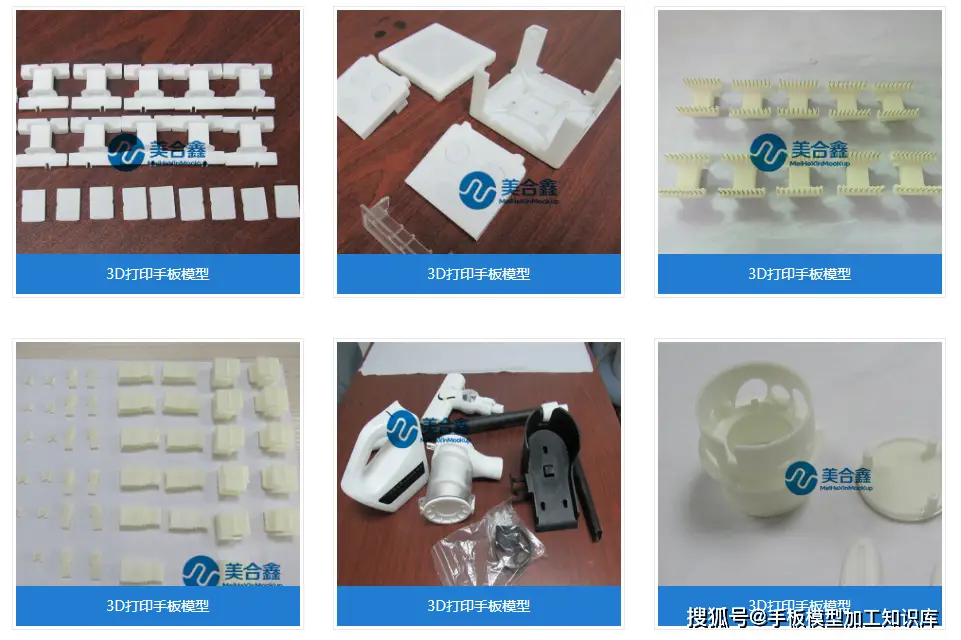
Innovative designs for consumer electronics and smart wearable devices are among the applications for 3D printing of complex structures, small-batch production, rapid prototyping and visual validation prototypes. Complex robotic joints and bionic structures also fall within its scope of application. Medical device casings and personalised implants are likewise within its scope. Cultural and creative products, sculptural ornaments and toys are further areas of application. 3D-printed prototype models are also utilised in scenarios such as early-stage design validation, aesthetic evaluation, exhibition displays and patent applications.
III. Vacuum Casting (Silicone Moulding): A “Cost-Effective Solution” for Small-Batch Trial Production”
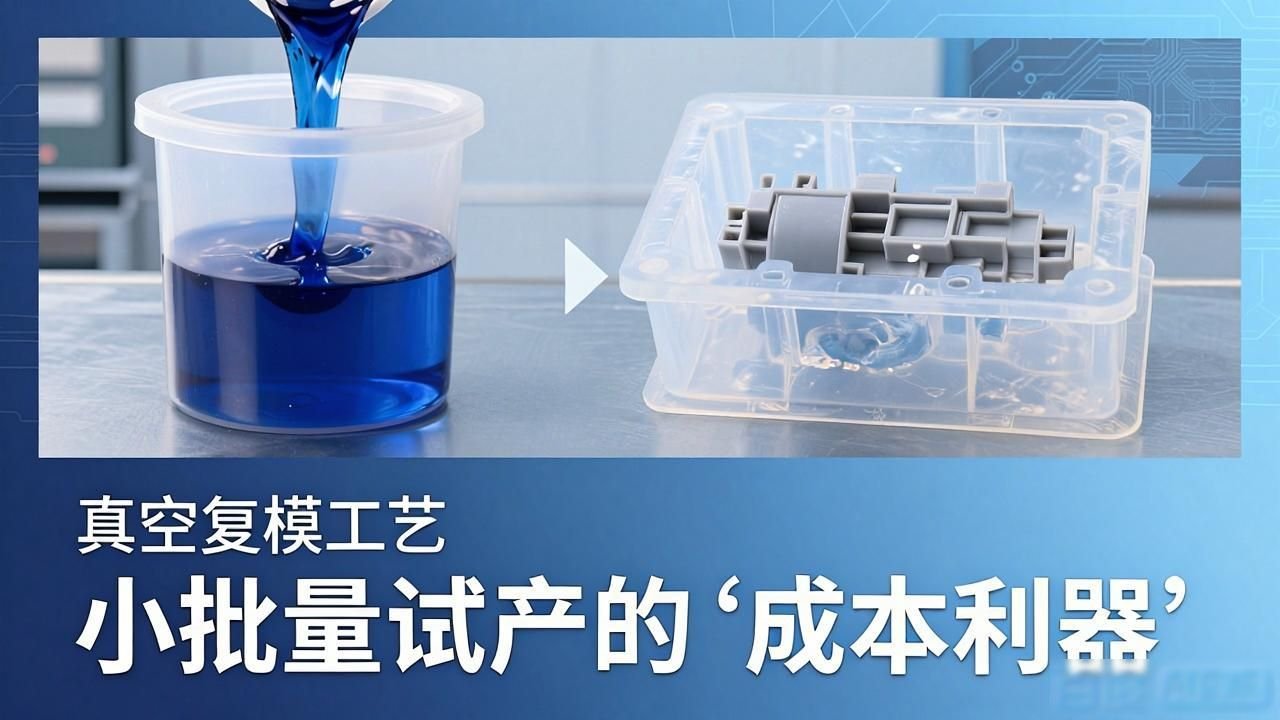
Vacuum casting, also known as silicone moulding, is a process used for the small-batch replication of prototypes. Its core process is as follows: first, a prototype is produced using CNC machining or 3D printing; next, the prototype is encased in silicone to create a flexible mould; subsequently, in a vacuum environment, liquid materials such as PU, ABS or soft rubber are injected into the mould; once the material has cured, the part is demoulded; finally, post-processing is carried out to produce the replicated part.
Key strengths:
For small-batch production runs of between 10 and 1,000 units, the costs are significantly lower than those of CNC single-piece machining and 3D printing. With low moulding costs and high replication efficiency, this method is suitable for companies conducting market testing as well as for small-batch trial production, offering the advantage of low-cost small-batch manufacturing.
Extremely efficient: a single silicone mould can produce between twenty and fifty items; the production cycle is very short, with batch production completed within two to three days, enabling rapid fulfilment of small-batch orders.
There is a wide variety of materials available, including hard plastics that can be replicated, soft plastics, transparent materials and high-temperature-resistant materials, amongst others. Their feel and texture are similar to those of mass-produced products, enabling them to meet assembly requirements whilst also fulfilling functional testing criteria.
The level of detail reproduction is very high; the silicone mould possesses excellent flexibility, enabling it to perfectly replicate the prototype’s fine textures, as well as text, grooves and other details; the replicas are highly consistent with the prototype.
Weaknesses and shortcomings:
There are certain limitations to the accuracy; replication accuracy is approximately plus or minus 0.1 to 0.3 millimetres, which is lower than that of CNC machining, and slight errors may occur during batch production.
Silicone moulds have a limited service life; they can often only be used between twenty and fifty times. In the case of mass production, this necessitates frequent replacement of the moulds, which makes their service life appear short.
Its performance is average; the properties of the moulding material lie somewhere between those of 3D-printed and CNC-machined parts, and its heat resistance and strength are somewhat lower than those of solid materials. Consequently, it is not suitable for use in tests requiring extremely high performance.
Use cases:
Vacuum casting is a method used for small-batch trial production—typically involving quantities of just 10 to 1,000 units—for market testing, and is also the preferred choice when rolling out products. It is primarily used in the following areas: for small-batch trial production of household appliance casings; for small-batch trial production of digital accessories; in the batch production of automotive interior components; in the batch production of automotive aftermarket parts; and in the batch production of medical device casings and medical device consumables; for the small-batch launch of cultural and creative products; for the small-batch launch of toys; as well as for scenarios such as market testing of new products, exhibition samples and bespoke customer orders, amongst others.
 Chinese
 Japanese
 English
 German
 Finnish
Leave a Reply
You must be logged in to post a comment.